Metal · 2 min read
Sanding metal: rust, welds, paint prep
Removing rust and mill scale, dressing welds, keying bare metal for primer – which grit for what, and how to tell it is too coarse.
Last updated: · published
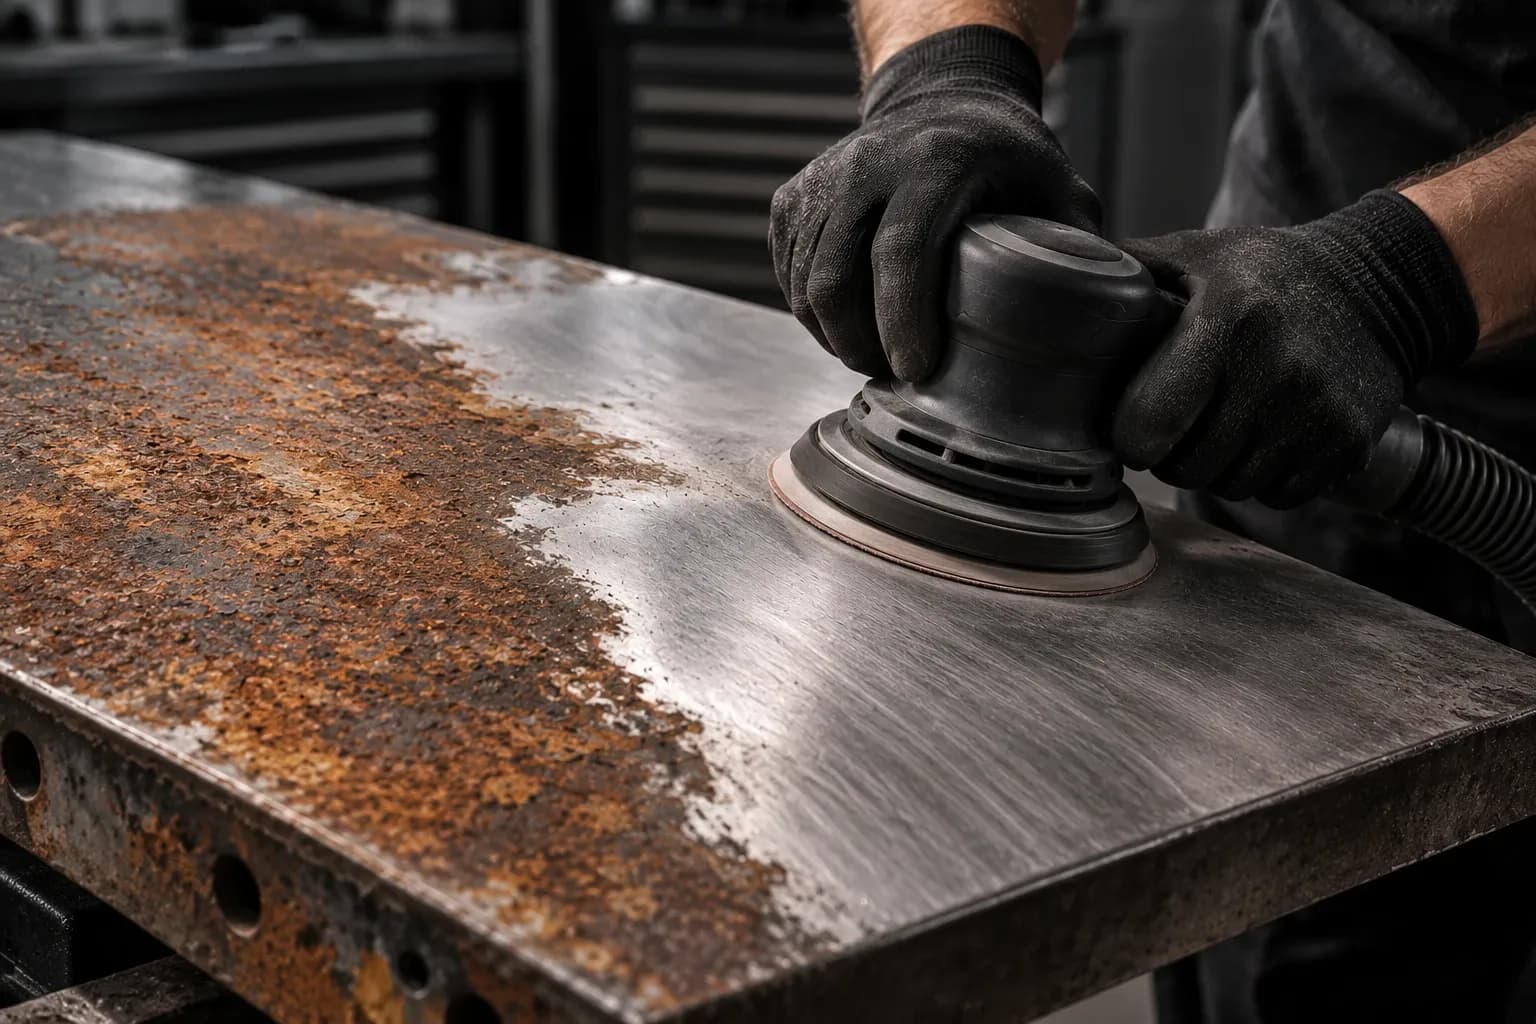
Rust and mill scale: P40 to P80
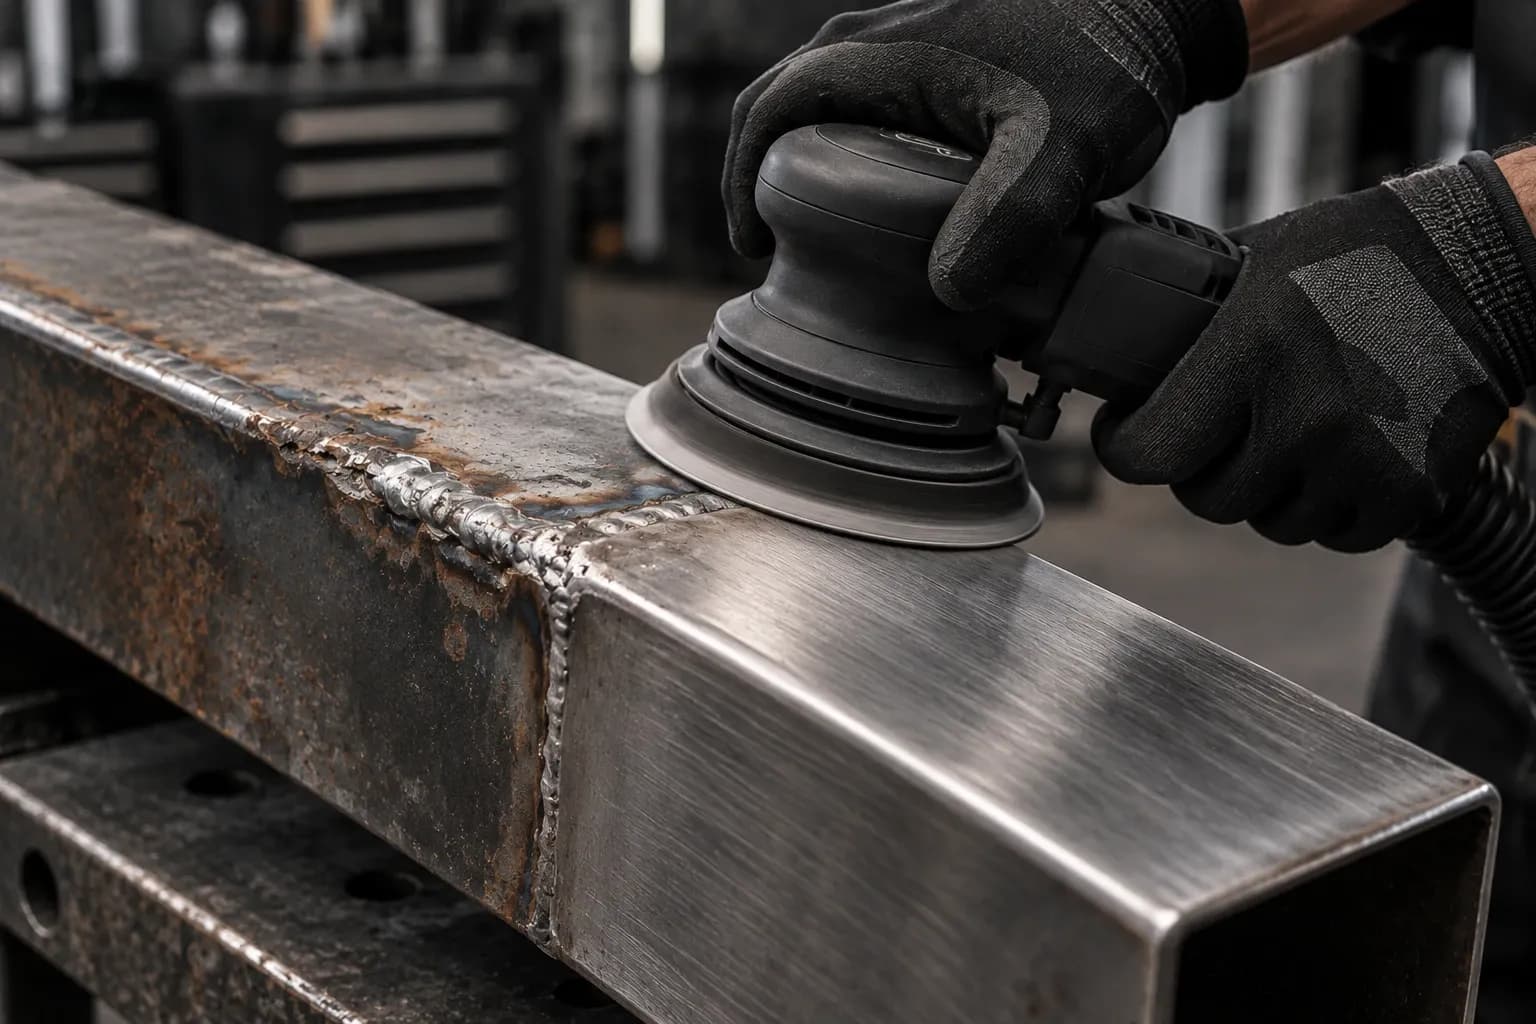
Widespread rust and mill scale need stock removal: P40 to P60 on a random orbital sander with a large orbit, or a flap disc on the angle grinder. Sand until bare metal remains with no brown spots – otherwise rust pockets in the pores come back under the paint.
Then remove the deep scratches with P80. Where the machine cannot reach, non-woven abrasive by hand does the job.
Welds and edges: P60 to P120
Grind the weld flush with P60 first, without going into the surrounding panel – otherwise the metal gets thin and warps from the heat. Sand thin sheet in short bursts and let it cool. Break sharp edges with P120 so the paint does not pull away there.
Keying for primer and paint: P120 to P240
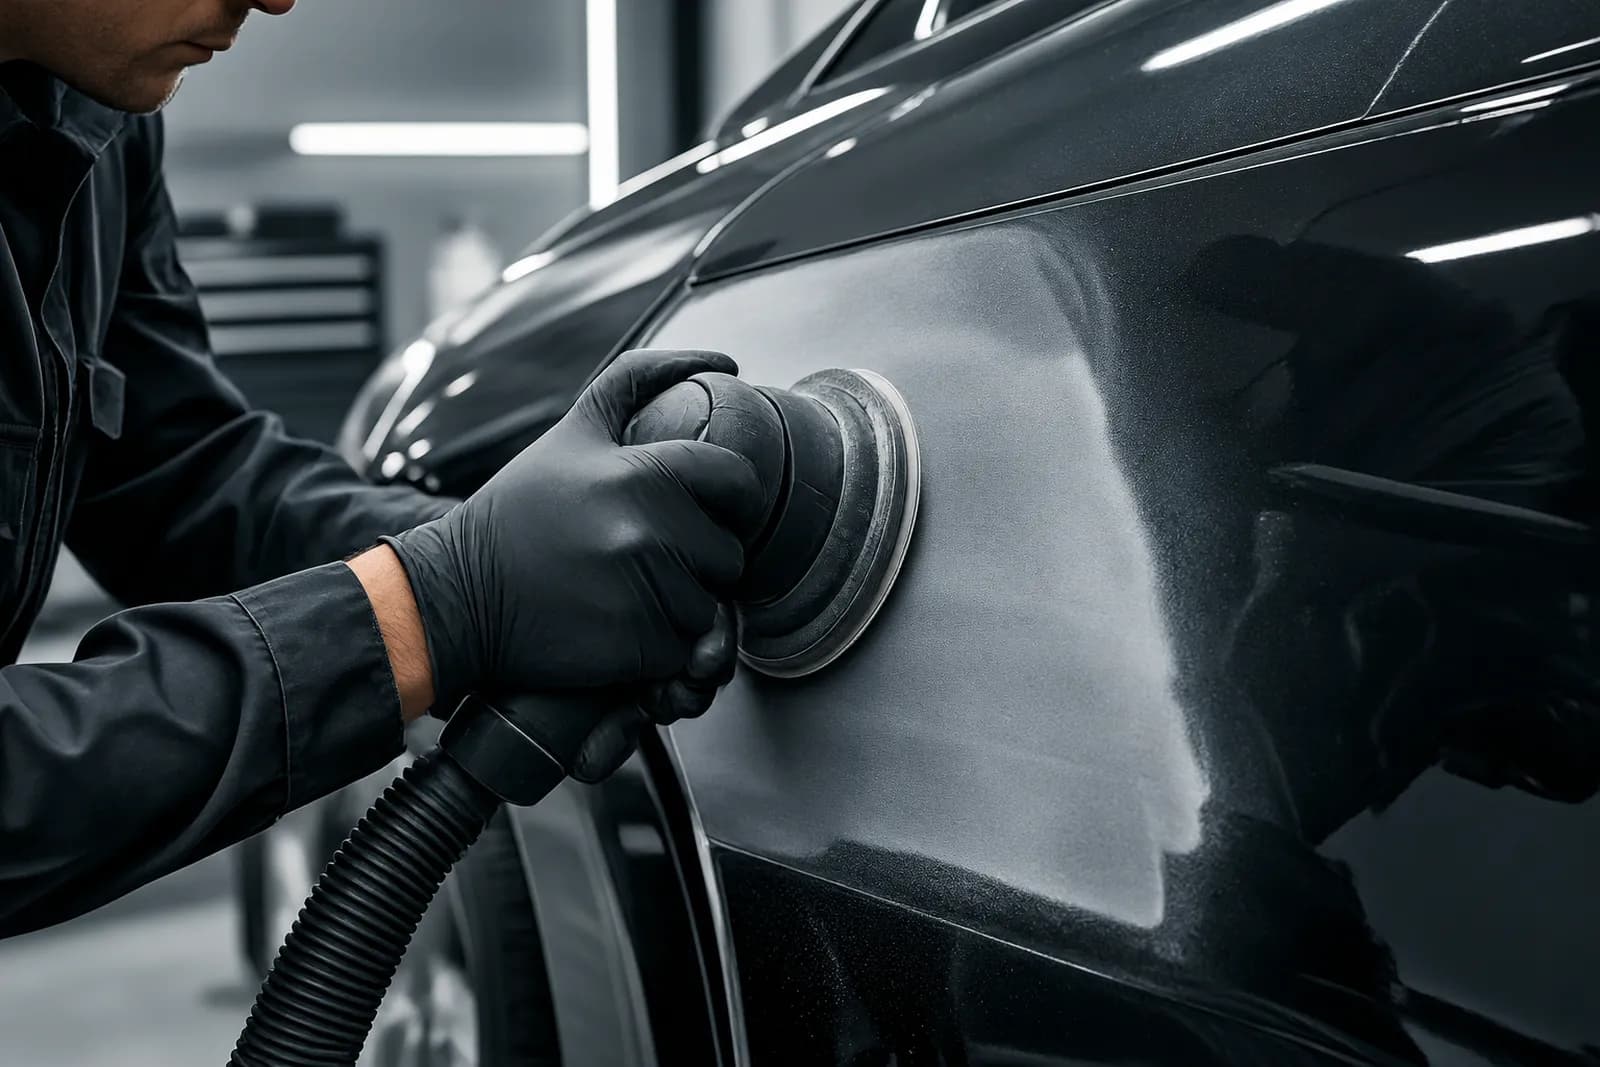
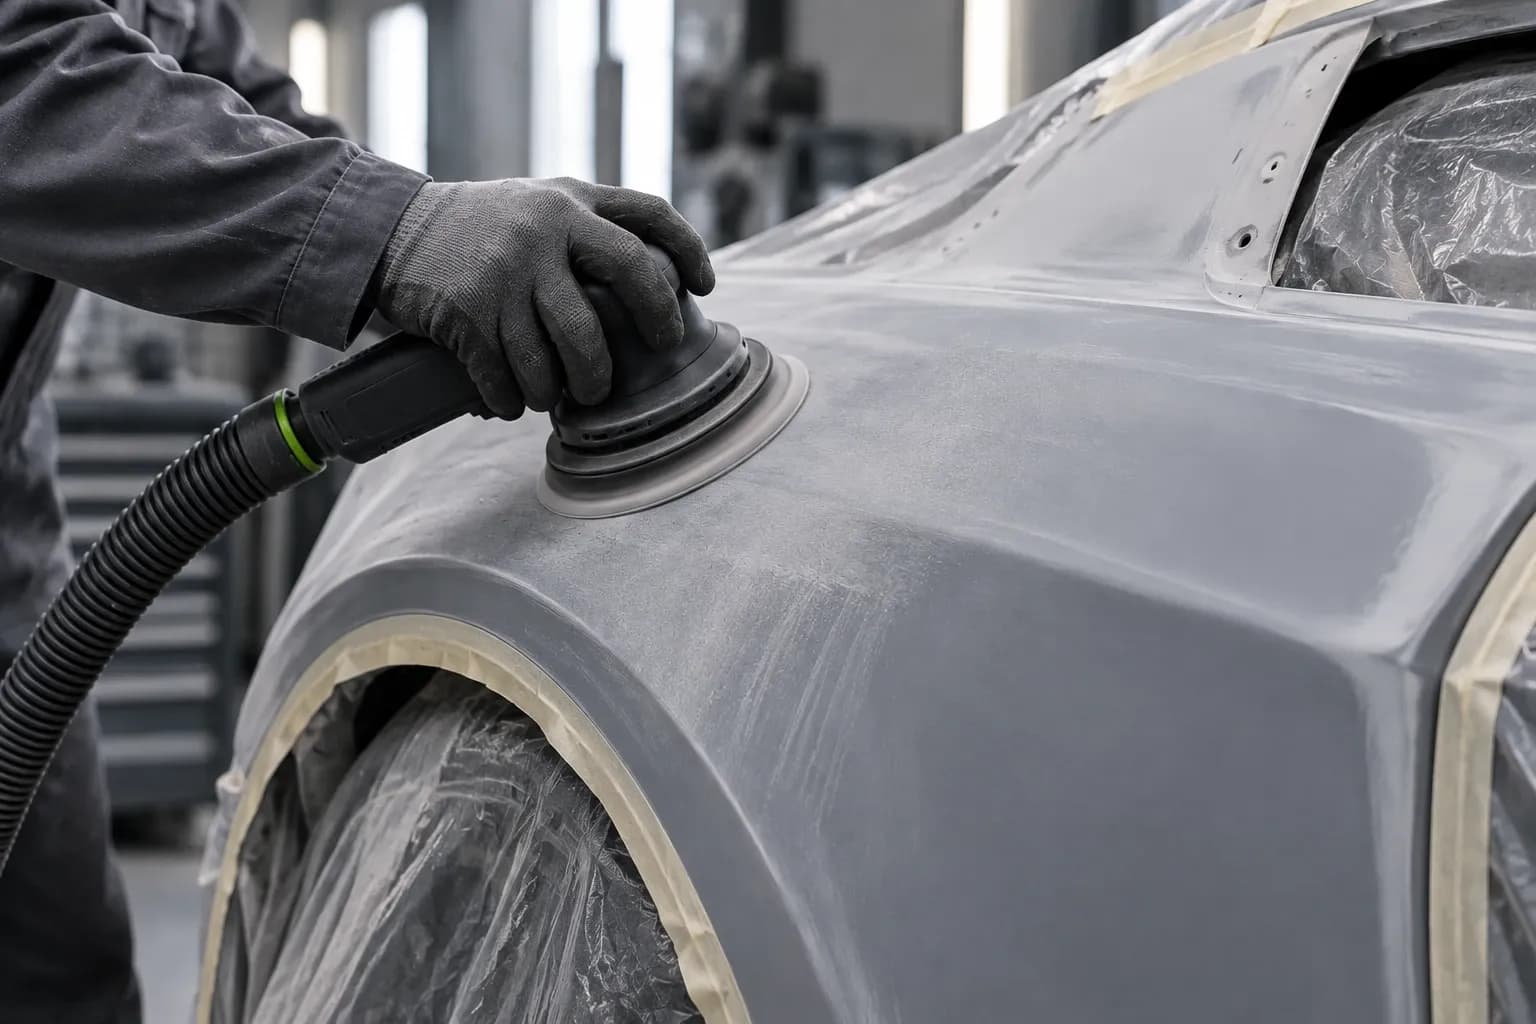
For a good key, bare metal needs an even scratch pattern with P120 to P180; under primer surfacer and body filler it can be coarser, under direct-to-metal paint more like P240. Then degrease and prime promptly – bare steel will flash-rust overnight.
Even finish: P240 to P400
Stainless steel and aluminium that stay visible get a consistent scratch pattern with P240 to P400 or with non-woven abrasive – always in one direction. Use dedicated abrasives for stainless that have never touched ordinary steel: iron particles otherwise cause contamination rust.
Random orbital sander or angle grinder?
The angle grinder with a flap disc removes material fastest – for welds, heavy rust and profiles. On thin body panels, however, it puts a lot of heat into a small spot; the panel distorts and is very hard to straighten again.
For flat areas, transitions and keying before primer, the random orbital sander is the better choice: it spreads the heat, leaves an even scratch pattern and, with dust extraction, works almost dust-free.
Working safely
Safety glasses are a must, and with an angle grinder also ear protection and gloves. Sparks fly a long way: keep anything flammable well away, and cover glass, paint and chrome – hot particles burn into them.
Old coatings can contain lead or chromium. When sanding off old paint, use dust extraction and wear at least an FFP2 dust mask.
FAQ
Which abrasive for steel?
For steel, aluminium oxide discs are the norm – tough and sharp for a long time. Coarse for rust and mill scale (P40 to P80), P120 to P240 for keying.
Do I have to prime immediately after sanding?
Yes, ideally the same day. Bare steel flash-rusts even at normal humidity.
Terms in this article
- Orbit (stroke)
- Deep scratches
- Abrasive fleece
- Primer surfacer
- Flash rust
- Scuff sanding (keying)
- Dust extraction
The whole sequence at once
3 grits, 1 × smallest pack each: PRO CUT 150 (10 pcs) P120 · P240 · P400. We don’t stock P60 for this yet. P60 is available for 125 mm backing pads as PRO CUT 125.
incl. VAT, plus shipping